
Custom electronic parts not only protect electronic parts but also need to support time and lower the usual costs included. They also have to support PCBs, withstand working temperatures, and ensure uniform dimensions throughout production.
HingTung, a China-based plastic injection molding manufacturer established in 2011, unifies design for manufacturing (DFM), injection molding and assembly within one workflow. This approach can ensure the right demands fit into the workflow.
Keep reading to explore custom plastic components for electronics along with their materials, manufacturing and OEM design.
Electronic products hold many plastic parts that rarely catch attention until something fails to fit or assemble correctly.
| Component | Typical Application | Main Design Concern |
| Electronic enclosures | Control units, instruments, IoT devices | Wall thickness and assembly fit |
| Connector housings | Electrical and cable connections | Contact positioning and insulation |
| PCB mounting brackets | Internal electronic assemblies | Boss strength and dimensional accuracy |
| Battery covers | Portable electronic products | Snap-fit durability |
| Control panels | Switches and electronic interfaces | Surface finish and appearance |
| Cable guides | Wire management | Retention and edge design |
| Plastic gears and supports | Mechanical assemblies | Wear and dimensional stability |
For a simple cover, material and surface finish may govern the discussion. For a connector housing, small dimensional changes can impact electrical contact alignment.
This is why experienced custom plastic parts manufacturers usually ask about the entire assembly, not just the single plastic part.
Also, learn how to improve quality in plastic injection molding.
A component that works as a prototype is not automatically ready for production. Manufacturing method affects tolerances, material behavior, surface lustre, and total cost.
| Method | Best For | Main Advantage | Limitation |
| 3D Printing | Early prototypes and small quantities | No customized tooling | Properties and finish vary by process |
| CNC Machining | Functional prototypes and precision parts | Good dimensional control | Higher machining prices for complex parts |
| Injection Molding | Repeatable OEM production | Simple production at sufficient volume | Upfront mold investment |
| Thermoforming | Covers, trays, and shallow panels | Highly simple tooling | Limited integrated features |
For early designs, CNC machining or 3D printing can help verify fit and accuracy. Once the design stabilizes and volume increases, injection molding often emerges as the more economical path.
Where HingTung fits: Its manufacturing team can review a recommended molded part before tooling begins, identifying issues such as unnecessary undercuts, difficult lifting, uneven walls, or problematic gate locations. Addressing these early is usually less pricey than changing a finished mold.
Choosing resin based only on cost is potentially hazardous. Electronic products may face heat, impact, mechanical stress, moisture, or regular assembly.
| Material | Key Characteristics | Typical Applications |
| ABS | Damage resistance and good surface appearance | Housings and control panels |
| PC | High impact strength and toughness | Protective surfaces and durable enclosures |
| PC/ABS | Balance of quality and processability | Electronic equipment housings |
| PBT | Electrical properties and remarkably low moisture absorption | Connectors and insulating components |
| PA6 / PA66 | Mechanical reliability and wear resistance | Brackets, clips, and mechanical parts |
| POM | Low friction and dimensional stability | Gears and moving components |
For example, ABS is often accepted for indoor equipment housings. PC or suitable PC/ABS grades may be more helpful where higher impact resistance is needed.
Material selection must still be determined at the grade level. Flame-retardant ratings, electrical properties, operating temperature, and environmental performance vary between commercial formulations.
HingTung can coordinate material purchase discussions with the mold design and manufacturing process, which is worthwhile when a material change also affects shrinkage, tooling dimensions, or the component fit.
For an OEM electronic product, tooling and production should not be perceived as unrelated purchasing actions.
HingTung provides integrated plastic injection molding and assistant manufacturing services, with a 50,000 m² manufacturing production site, more than 350 pieces of equipment, and over 80 injection molding machines with clamping sizes up to 650 tons.
Its process description covers DFM, mold development, injection molding, CNC machining, secondary processing, inspection, and final installation.
Set up a plastic housing with internal PCB supports, threaded inserts, and a replica cover.
During trial molding, the cover may show slight warpage or the assembly bosses may not align exactly with the PCB. If tooling and molding teams work differently, correcting the issue can involve several rounds of discussion.
With in-house tooling and molding oversight, HingTung can review trial results, adjust mold features, and verify additional molded samples within a connected process.
This does not minimize engineering changes, but it can reduce unnecessary handoffs between traders.
Some OEM projects include multiple plastic components, secondary machining, fastener installation, or final set-up.
HingTung’s supporting services make it possible to perform these steps alongside injection molding, rather than requiring every process to be managed as a discrete sourcing task.
For electronics manufacturers, the benefit is not purely a lower molded-part price. It is more consistent cooperation between tooling, production, quality inspection, and the finished assembly.
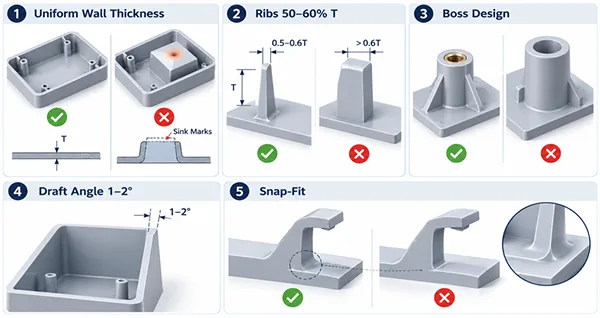
Plastic element design is often where the biggest manufacturing problems begin. A model may look perfect in CAD but still create sink marks, distortion, or assembly headaches.
Uniform wall thickness helps maintain steady cooling. Thick sections around bosses and ribs can cause sink streaks or internal voids.
For many injection-molded parts, rib thickness around 50–60% of the proposed wall is a useful starting point. The final dimensions depend on the resin, geometry, and design requirements.
Screw bosses should also be engineered around the intended fastener and assembly load, not simply made as thick as required.
For OEM components, HingTung’s DFM process helps highlight these issues before mold manufacturing, when changes are easier to execute.
Draft angles ensure reliable part ejection. Around 1–2° per side is a common starting point for smooth surfaces, although texture, part depth, and material may need changes.
Snap-fits need careful analysis of strain, root radius, material behavior, and proposed assembly cycles.
A snap arm that is functioning during the first assembly is not normally suitable for repeated opening over several years.
Also, learn about Fibre Optic Cabling for reliable uptime.
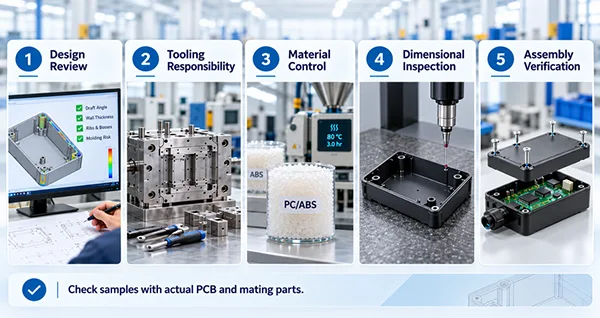
Machine capacity matters, but it is only one phase of supplier evaluation.
I would ask a potential custom plastic parts manufacturer to talk about how it handles the following:
HingTung’s integrated manufacturing model is needed here because mold corrections, molding adjustments, and inspection complaints can be managed within the same production technique.
For electronic enclosures, I would also ask for samples assembled with the actual PCB, fasteners, and mating attachments. A dimensional report is useful, but real assembly testing can reveal problems that individual part measurements miss.
The lowest unit price is not generally the minimum project cost.
A supplier may quote an attractive molding price while tooling tweaks, secondary machining, assembly, and inspection are performed separately.
For custom plastic pieces, the full calculation should include machine costs, material, molding cycle time, scrap, finishing, assembly, examination, and logistics.
Three areas should receive early attention:
This is where a manufacturer such as HingTung can offer a tactical advantage. Keeping mold development and production closely connected makes it easier to investigate the effects of design changes on the overall manufacturing process.
In the end, effective custom plastic components start with careful planning. Choosing material, tooling demands, and assembly tolerances can all affect product quality and manufacturing costs. Considering these aspects in time can help to lower defects and avoid costly production charges.
HingTung provides this process with coordinated DFM, mold manufacturing, injection molding, and supporting operations, making it a practical choice. For OEM projects, this combined approach can ease supplier coordination and help ensure uniform quality from initial design through production.
Ans: Yes, where the application authorises. Recycled-content grades should be assessed for consistency, mechanical performance, appearance, traceability, and useful electrical or regulatory conditions.
Ans: Yes. Metal inserts can be contained during molding or installed afterwards using appropriate insertion methods. The choice depends on pull-out strength, torque provisions, part geometry, and production magnitude.
Ans: A 3D CAD model, magnitude drawing, material specification, counted production volume, cosmetic requirements, and any critical dimensions provide a useful starting point.
Ans: Gate position, resin drying, mold temperature, packing requirements, and surface finish all affect appearance. Approved study samples and defined review criteria help maintain consistency.
