
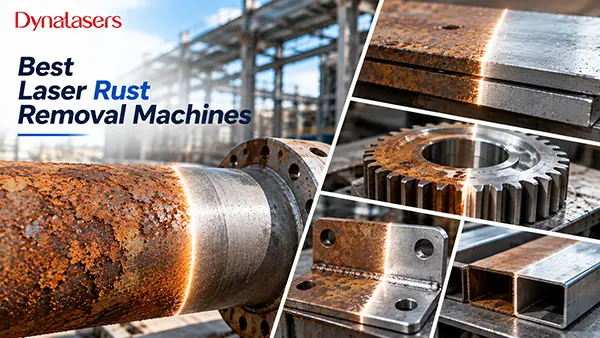
Rust may make important equipment in the industry difficult to maintain due to slow production and costly surface preparation.
Sandblasting and other traditional processes may get the job done, but they might generate additional waste, need thorough cleanup, or be hard to apply in tight spaces. This is when laser cleaning comes into play. Not all laser rust removal machines will cope well with thick rust, large steel structures, and high-precision parts.
In this guide, we compare seven options based on cleaning performance, laser technology, portability, and practical applications, including Dynalasers M75 and P300.
| Manufacturer | Representative System | Laser Technology | Main Strength | Suitable For |
| Dynalasers | M75 / P300 | CW / MOPA pulsed | Compact air-cooled options | Heavy rust and controlled cleaning |
| IPG Photonics | CL 500iM | 500W pulsed | Portable integrated cleaning system | Industrial maintenance |
| Laserax | LXQ-HP Series | High-power pulsed fiber laser | Automated process integration | Production-line rust removal |
| Laser Photonics | CleanTech CR-3010 | CW fiber laser | Industrial surface conditioning | Steel maintenance and refurbishment |
| P-Laser | QF Series | Pulsed laser | Controlled surface treatment | Localized industrial cleaning |
| SENFENG | HC Series | CW / pulsed options | Multiple industrial configurations | General metal cleaning |
| GWEIKE | LC Series | Fiber laser cleaning | Workshop-oriented equipment | Rust and coating removal |
A laser rust cleaning device should be judged by the type of corrosion it can remove consistently, not just maximum wattage.
A high-power cleaner is helpful for large steel surfaces, while a pulsed machine may be more appropriate when the underlying material must retain a particular finish.
Dynalasers provides two methods of removing rust on industrial materials. The M75 utilizes continuous-wave laser output for larger cleaning jobs, while the P300 uses MOPA pulsed technology for more controlled surface treatment.
Both use forced-air cooling, avoiding a separate water-chiller circuit. That makes them more manageable and easier to move around workshops and industrial maintenance sites.
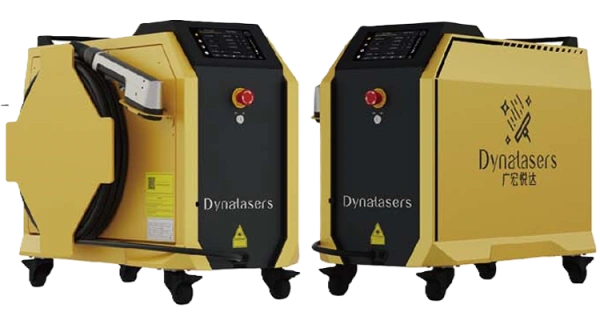
The Dynalasers M75 continuous laser cleaner is the more logical starting point when a large amount of corrosion needs to be removed.
Its CW laser delivers output up to 1800W. The machine weighs less than 43 kg and contains a 10-meter cable, making it practical for cleaning large components without constantly repositioning the cabinet.
With the F800 lens, the cleaning width can reach 300 mm. This is beneficial when working on steel plates, structural frames, machinery, and other relatively large surfaces.
I would consider the M75 for:
The higher average power helps with bulk removal, but it also introduces more heat into the surface. Scan speed, overlap, focus, and the condition of the steel need cautious adjustment.
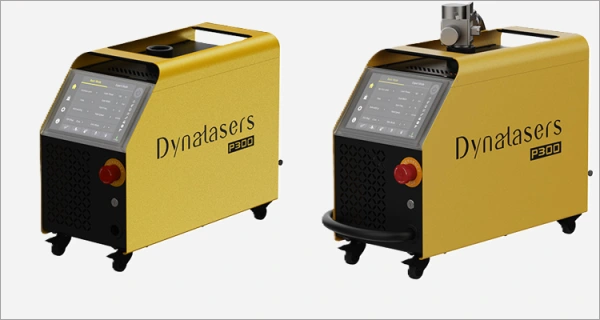
The P300 pulse laser cleaner addresses a different issue. It uses a 300W-class MOPA pulsed fiber laser and weighs less than 25 kg.
Instead of continuous energy delivery, the P300 uses controlled laser pulses. Its selectable pulse-energy configurations and dual-axis scanning provide flexibility when treating smaller or more sensitive surfaces.
I would look at this device for localized oxidation, machined components, mold surfaces, and parts where excessive heating or roughening would be unacceptable.
The P300 is not necessarily quicker than the M75. For thick rust over several square meters, a CW system often makes more sense. But when surface condition matters more than bulk removal speed, pulsed cleaning deserves consideration.
One blunder in industrial rust removal is treating all visible corrosion as the same trouble.
Light surface oxidation may disappear in a single pass. Thick, flaky rust can demand slower scanning, multiple passes, and more careful inspection.
| Rust Condition | Typical Challenge | Practical Approach |
| Light surface rust | Avoiding unnecessary substrate heating | Controlled pulsed cleaning |
| Moderate rust on steel | Balancing speed and cleaning quality | CW or pulsed cleaning |
| Thick, layered corrosion | Removing material through several layers | Higher-power CW, multiple passes |
| Rust around welds | Reaching irregular geometry | Narrower scan patterns and repositioning |
| Precision components | Preserving dimensions and surface finish | Carefully tested pulsed cleaning |
The laser rust removal process cannot rejuvenate steel that has already corroded to an extent of losing some of its material. It removes the corrosion products, but pitting and reduced wall thickness remain.
That distinction matters for pressure vessels, load-bearing structures, and safety-critical machinery. Cleaning should not be confused with structural repair.
For most workshops, the choice comes down to how much rust requires removing and what condition the metal must be left in.
| Requirement | M75 CW | P300 MOPA Pulsed |
| Large steel structures | Preferred | Generally slower |
| Heavy surface corrosion | Preferred | Possible with multiple passes |
| Light localized rust | Suitable | Preferred |
| Precision metal components | Requires careful testing | Preferred |
| High-throughput cleaning | Preferred | Application-dependent |
| Sensitive surface finishes | Greater thermal risk | Better control potential |
The P300 offers more flexibility in pulse-based cleaning, but that does not guarantee zero surface damage. Both machines need parameters developed around the actual material.
For a rusty steel frame, I would normally start with the M75. In cases of machined components in which surface texture is important, the P300 will be my initial choice to test on.
A laser rust remover can eliminate abrasive media and decrease the need for masking in some applications. It also allows localized cleaning without physically contacting the workpiece.
However, that does not make laser cleaning the most suitable option for every surface.
| Factor | Laser Cleaning | Sandblasting |
| Localized rust removal | Precise and selective | Requires more masking |
| Large open surfaces | Depends on rust thickness and power | Often highly productive |
| Surface roughness | Can preserve or modify texture | Creates an abrasive profile |
| Consumables | No blasting media | Requires abrasive media |
| Waste handling | Fumes and captured particles | Spent abrasive and contamination |
| Complex recesses | Limited by beam access | Media can reach some difficult areas |
If the specified coat necessitates an anchor profile to be provided, mere removal of rust that is visibly present using a laser would not suffice.
I would check the required surface cleanliness, roughness, and coating manufacturer’s recommendations before deciding to replace abrasive blasting.
A supplier demonstration should use the customer’s actual corroded material. A lightly oxidized sample plate rarely represents years of corrosion on industrial equipment.
Before choosing a portable laser rust removal machine, I would check:
Ask the supplier to record the cleaning parameters and number of passes. A single cleaning-speed figure means little without knowing the original surface condition.
Fume extraction and laser safety also need attention. Rust and old coatings produce airborne particles during removal, and unknown paints may contain hazardous substances.
A well-controlled working environment, appropriate protective gear, and proper extraction is necessary.
The best laser rust removal machine depends on corrosion thickness, cleaning area, and the condition required after treatment. A machine that works well on heavy steel structures may not be the right choice for precision components.
Dynalasers covers both needs with the M75 for higher-throughput CW cleaning and the P300 for controlled pulsed treatment. The final choice should be based on actual rust removal trials, not maximum laser power alone.
Ans: It can remove accessible corrosion products, but it cannot rebuild metal lost through pitting. Severely corroded structural parts may require thickness measurement, repair, or replacement.
Ans: Yes, but the cleaned surface must meet the coating system’s preparation requirements. Additional surface profiling or chemical pretreatment may still be necessary.
Ans: Moisture can affect energy absorption, cleaning consistency, and contamination behavior. Drying the surface before cleaning is generally preferable, particularly when repeatable results are required.
Ans: It can. Bare carbon steel can oxidize again when exposed to moisture and oxygen. Appropriate drying, protective coating, or another corrosion-control step should follow cleaning.
